 English EN
 Germany DE
 French FR
 Portuguese PT
 Spanish ES
X-Ray Inspection for Packaged Food Products
Packaged food X-ray inspection examines sealed products without opening the pack. It can identify foreign contaminants and, where the product and system support them, check conditions such as missing components, fill level, product integrity and material in the seal area.
A suitable packaged food inspection system must match the product and its package. Pouches, cartons, foil trays, bottles, cans and jars produce different X-ray images and require different mechanical and imaging configurations. RaymanTech offers X-ray inspection systems for food that can be evaluated for these line conditions.
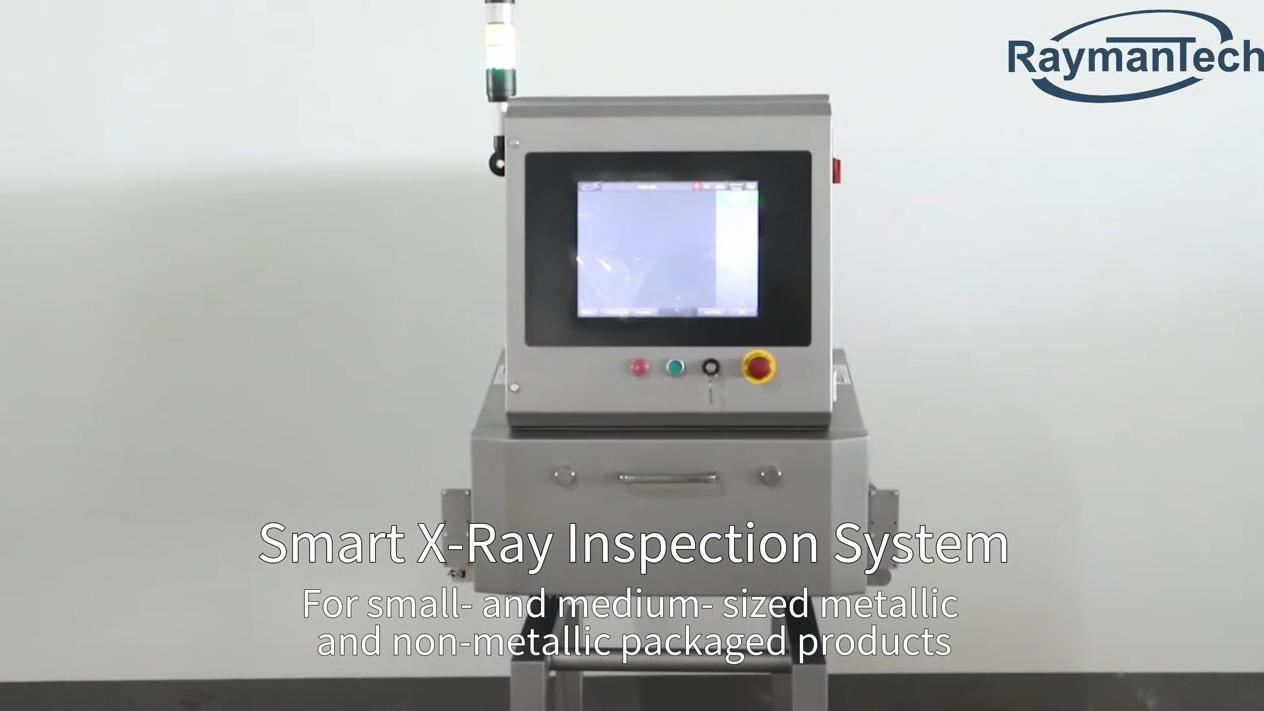
Key point: Detector resolution or X-ray power alone does not define performance. Product density, package structure, target material, line speed, imaging geometry and software settings work together and must be tested as one application.
How X-Ray Inspection Works on a Packaging Line
After filling and sealing, the conveyor moves each pack through a shielded inspection chamber. X-rays pass through the food and packaging. A detector records the transmitted energy and creates an image based on absorption differences.
Product program: The system loads settings for the product and package format.
Image acquisition: The generator and detector capture the internal product image.
Inspection decision: Software evaluates configured contaminant and quality criteria.
Reject action: A nonconforming pack is removed and the event can be recorded.
What Can a Packaged Food Inspection System Detect?
Not every low-density contaminant or packaging defect is visible to X-ray. A hazard assessment should define what the system is expected to detect and what must be controlled by another method.
Packaging Formats and Their Inspection Considerations
For tray-based convenience products, see the application guide for ready meal X-ray inspection. For rigid containers, review solutions for the canned, jarred and bottled food industry.
Why X-Ray Is Used with Foil Packaging
Conventional metal detectors use an electromagnetic field, so aluminum foil or metallized film can affect the inspection response. X-ray inspection uses a different principle. It measures how the complete product and package absorb X-rays, which allows metal and selected non-metal contaminants to be inspected in many foil-based packs.
The packaging is still part of the X-ray image. Thick seams, closures, clips or overlapping layers can create dense areas, so testing must include the final commercial pack rather than the food alone.
How to Choose a Packaged Food X-Ray System
Product and package: Record dimensions, weight, density, orientation and package material.
Inspection target: Define relevant contaminants and any required quality checks.
Line conditions: Confirm conveyor speed, spacing, transfer points and available installation space.
Imaging configuration: Select the inspection direction and detector arrangement for the product geometry.
Reject handling: Match the reject device, confirmation sensors and reject bin to the package.
Hygiene and environment: Consider cleaning method, temperature, moisture and the required enclosure design.
Validation: Test normal product variation and target samples under representative operating conditions.
Avoid specification-only selection: A higher nominal resolution or power rating does not guarantee better results on your pack. Use a documented product test to compare detection capability, false rejects, throughput and reject reliability.
Packaged Food X-Ray Inspection FAQ
What can packaged food X-ray inspection detect?
It can detect metal and selected dense non-metal contaminants when sufficient contrast exists. Some applications also support checks for missing items, fill, integrity or material in a seal region.
Can X-ray inspect food in foil or metallized packaging?
Yes, many foil and metallized packs can be inspected because X-ray evaluates absorption rather than an electromagnetic field. The finished pack should be tested.
Where should the system be installed?
Many lines inspect after filling and sealing so the system evaluates the finished pack. The best point depends on contamination risks, required checks, space and reject handling.
How should a system be selected?
Evaluate the product, package, target contaminants, line speed, quality checks, installation space, hygiene conditions and reject arrangement, then confirm the configuration with representative tests.
Test Your Packaged Food Application
Share your product, package, target contaminants and line requirements with RaymanTech.
Related Articles
-
 Jan-23-2026
Introduction to RaymanTech Optical Sorters for Farm Products and Food Processors
RaymanTech, as a leading provider of inspection and sorting solutions, has developed a comprehensive optical sorter portfolio that now serves both farm-product applications and food-processing environments. While farm-product sorters focus on capacity, adaptability, and raw-material variability, food-processor-grade sorters must also incorporate high IP protection, robust stainless-steel construction, sanitary design, and harsh washdown compatibility.learn more -
 Jan-23-2026
How Safe is X-ray Inspection of Food?
Consumers and manufacturers alike worry about contamination in food – broken glass, metal fragments, plastic or stone – entering a product and harming someone or prompting a recall. X-ray inspection systems have become a key solution: conveyors carrying packaged or unpackaged food pass through a shielded X-ray machine that “sees” inside each item. This technology complements traditional metal detectors and manual checks to catch a wider range of hazards. Importantly, extensive research and industry experience show that food X-ray inspection is extremely safe. Nearly everything we eat – from spices to snacks – is X-rayed at some point during production, and regulatory bodies (like the FDA) report “no known adverse effects” from the low-dose X-ray scans used in food plants.learn more -
 Jan-23-2026
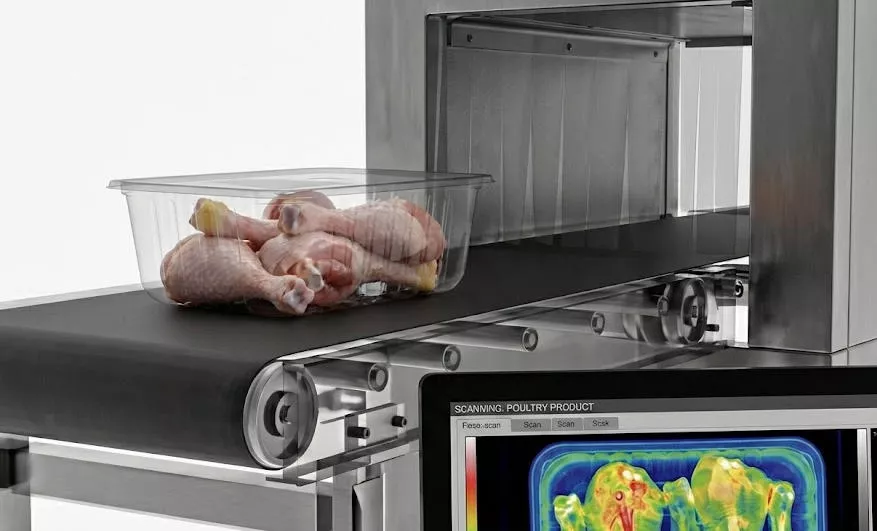
RaymanTech Fat Analysis X-Ray Inspection System for Poultry
X ray fat analysis enhances hidden contaminant detection in meat, ensuring safety, compliance, and accurate fat measurement for consistent product quality.learn more
Follow us:
